Automotive & Auto Parts
Lean production & quality
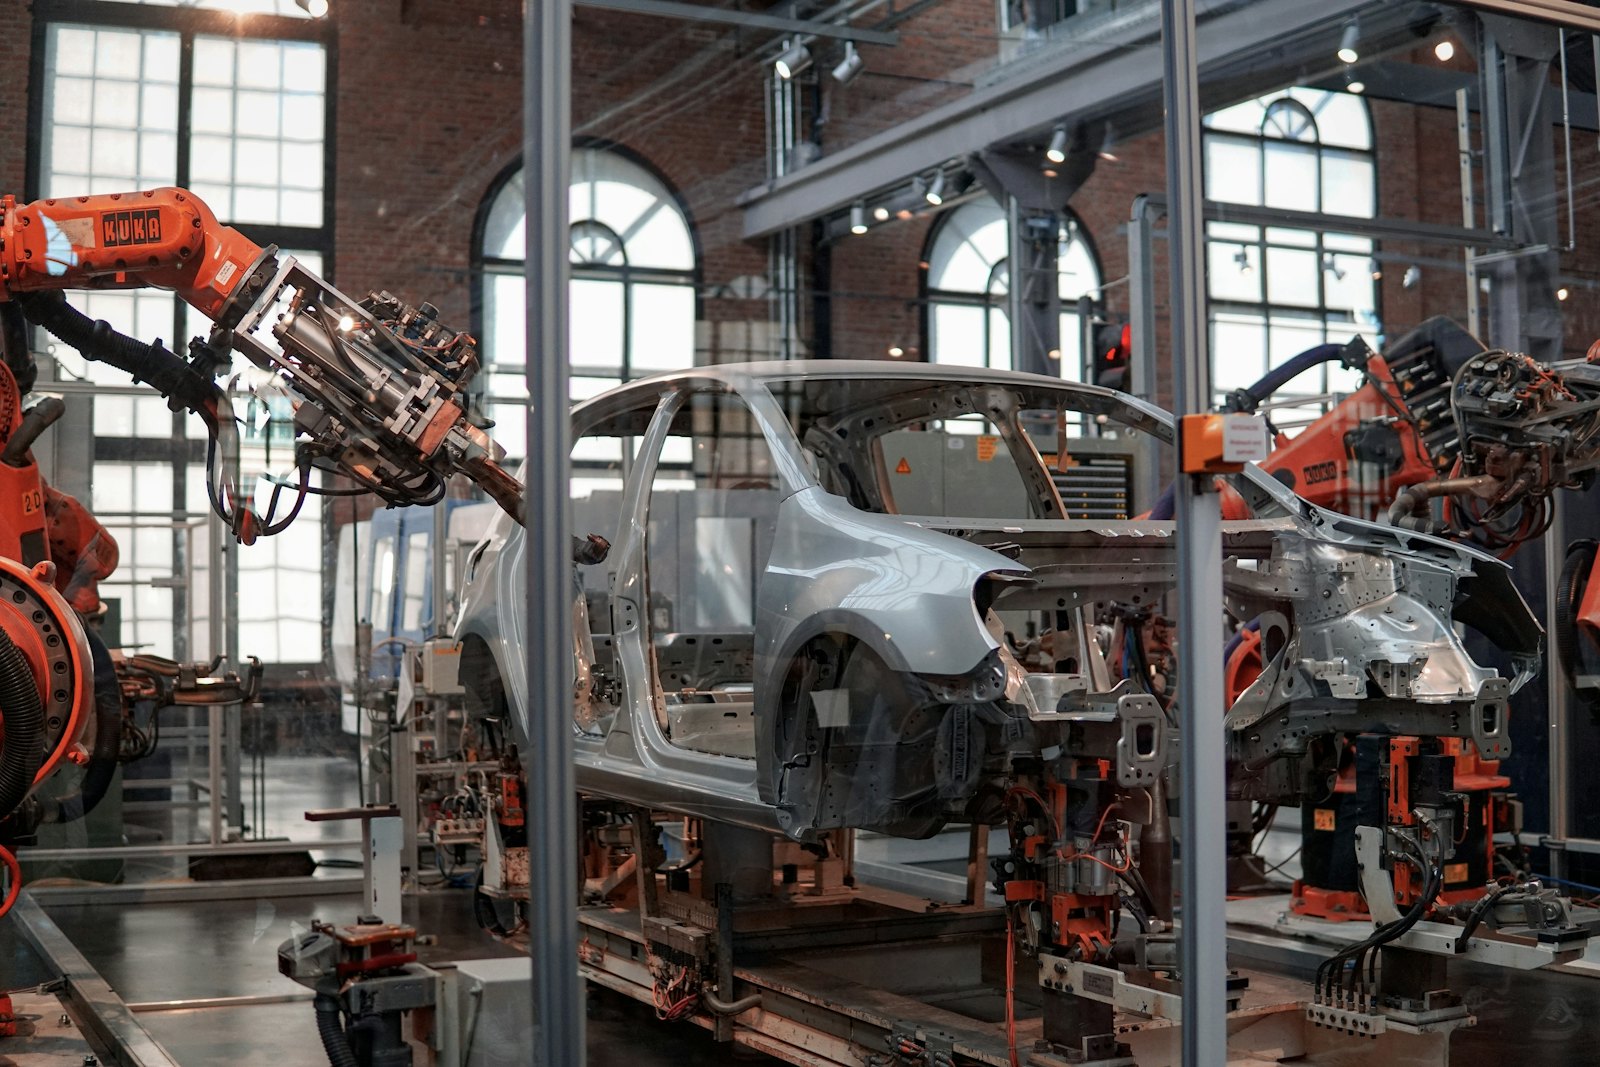
Automotive supply does not have one production problem. It has a changeover problem, a traceability problem and a schedule problem, and they argue with each other all day: every extra variant the customer asks for adds another changeover, every changeover pushes the schedule, and every schedule push creates pressure that shows up as quality problems.
We work mostly in tier-one and tier-two suppliers, where the customer sends a drawing and expects the same part at the same quality for years. That means a process that was settled years ago has to keep producing to a standard it was never designed for.
The improvements that pay in this industry are rarely glamorous. They are separating the change from the run, binding the process to the batch, and finding the defect at the station instead of at the end of the line.
What we know. This industry runs on long agreements, short notice and unforgiving audit requirements. A process that cannot show what it did last Tuesday is a process that cannot take a new customer. What we do not do. We do not replace the line, and we do not ask you to change your tooling. We work with the equipment and the people you already have.
What actually goes wrong in automotive supply
Five things, in the order they usually surface.
How we solve it
Three moves, in this order. The order matters: separating the change is what makes it possible to measure it, and measuring it is what makes binding the batch worth doing.
Once the changeover is defined, the second move follows naturally — every parameter that matters gets recorded against the batch, so a question about a part from six months ago can be answered. The third is structural: the station that can detect the defect becomes the station that reports it, instead of passing a suspicion down the line.
What this covers in practice
Area | What we address | What it changes for you |
Changeover & scheduling | Internal and external work separated, prepared ahead, executed as a routine | The line stops for a defined short period rather than an open one |
Traceability | Batch, material, shift, machine and parameters joined to the part | A returned part can be reconstructed without a week of searching |
In-process quality | Checks at the station that can actually stop the part | Defects contained at the point they occur |
Customer requirements | Drawing and process revisions handled as controlled changes | The floor and the customer specification stay together |
Supplier collaboration | Incoming material linked to the batch that consumed it | A supplier issue is scoped rather than argued about |
What we bring from this industry
Not a claim of coverage — what we have actually had to solve, and what that taught us.
How we deliver
Stage | What we do | What you get |
Assess | Watch a few changeovers and follow one batch through the process | A measured view of where the time and the risk actually sit |
Pilot | Redesign and rehearse one changeover with the line team | A defined routine, rehearsed by the people who will run it |
Bind | Attach parameters, material and shift to the batch | A part that can be reconstructed from its record |
Hold | Add station-level checks and change control, and keep them running | Quality and specification held by the process, not by memory |
What we solve
Each of these is something we take responsibility for solving, in this industry, on a working line.
How we work with you
Start with one changeover. The one that costs you most, measured on your own numbers.
Work with the line team. They design the routine; we make sure it survives contact with the schedule.
Keep the record with you. The traceability you build belongs to the plant, not to us.